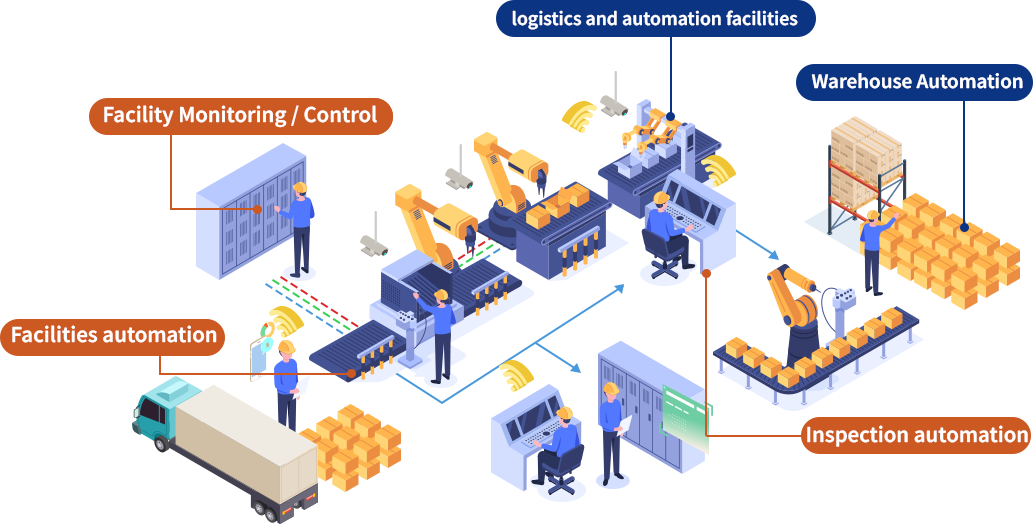
A smart factory is an intelligent production plant that applies information and communication technology to every stage of production — design, manufacturing, and distribution.
Innobase's differentiating strengths: with expertise and integration capabilities that solve the challenges of the manufacturing floor, we deliver faster and more reliable results.
Per the Ministry of Economy and Finance's definition, a "smart factory" is an intelligent production plant that applies information and communication technology (ICT) — combined with digital automation solutions — across the production process, including design/development, manufacturing, and distribution/logistics, to improve productivity, quality, and customer satisfaction.
In other words, it's a factory that connects its equipment and devices over wireless communication to monitor all data generated on the floor in real time, sharing and centrally managing that information. The collected data is analyzed using techniques such as machine learning and used to build the optimal production environment. Ultimately, it's a production system built on technologies such as the Internet of Things, big data, cloud computing, intelligent robots, and cyber-physical systems (CPS) — one where monitoring, maintenance, and management of the entire production process operate organically within a single network.
Converting a manufacturing operation to a smart factory delivers data-driven process monitoring and production informatization together as core solution features, with a range of additional features available to choose and adopt.
Per the Ministry of Economy and Finance's definition, a "smart factory" is an intelligent production plant that applies information and communication technology (ICT) — combined with digital automation solutions — across the production process, including design/development, manufacturing, and distribution/logistics, to improve productivity, quality, and customer satisfaction. In other words, it's a factory that connects its equipment and devices over wireless communication to monitor all data generated on the floor in real time, sharing and centrally managing that information. The collected data is analyzed using techniques such as machine learning and used to build the optimal production environment. Ultimately, it's a production system built on technologies such as the Internet of Things, big data, cloud computing, intelligent robots, and cyber-physical systems (CPS) — one where monitoring, maintenance, and management of the entire production process operate organically within a single network.
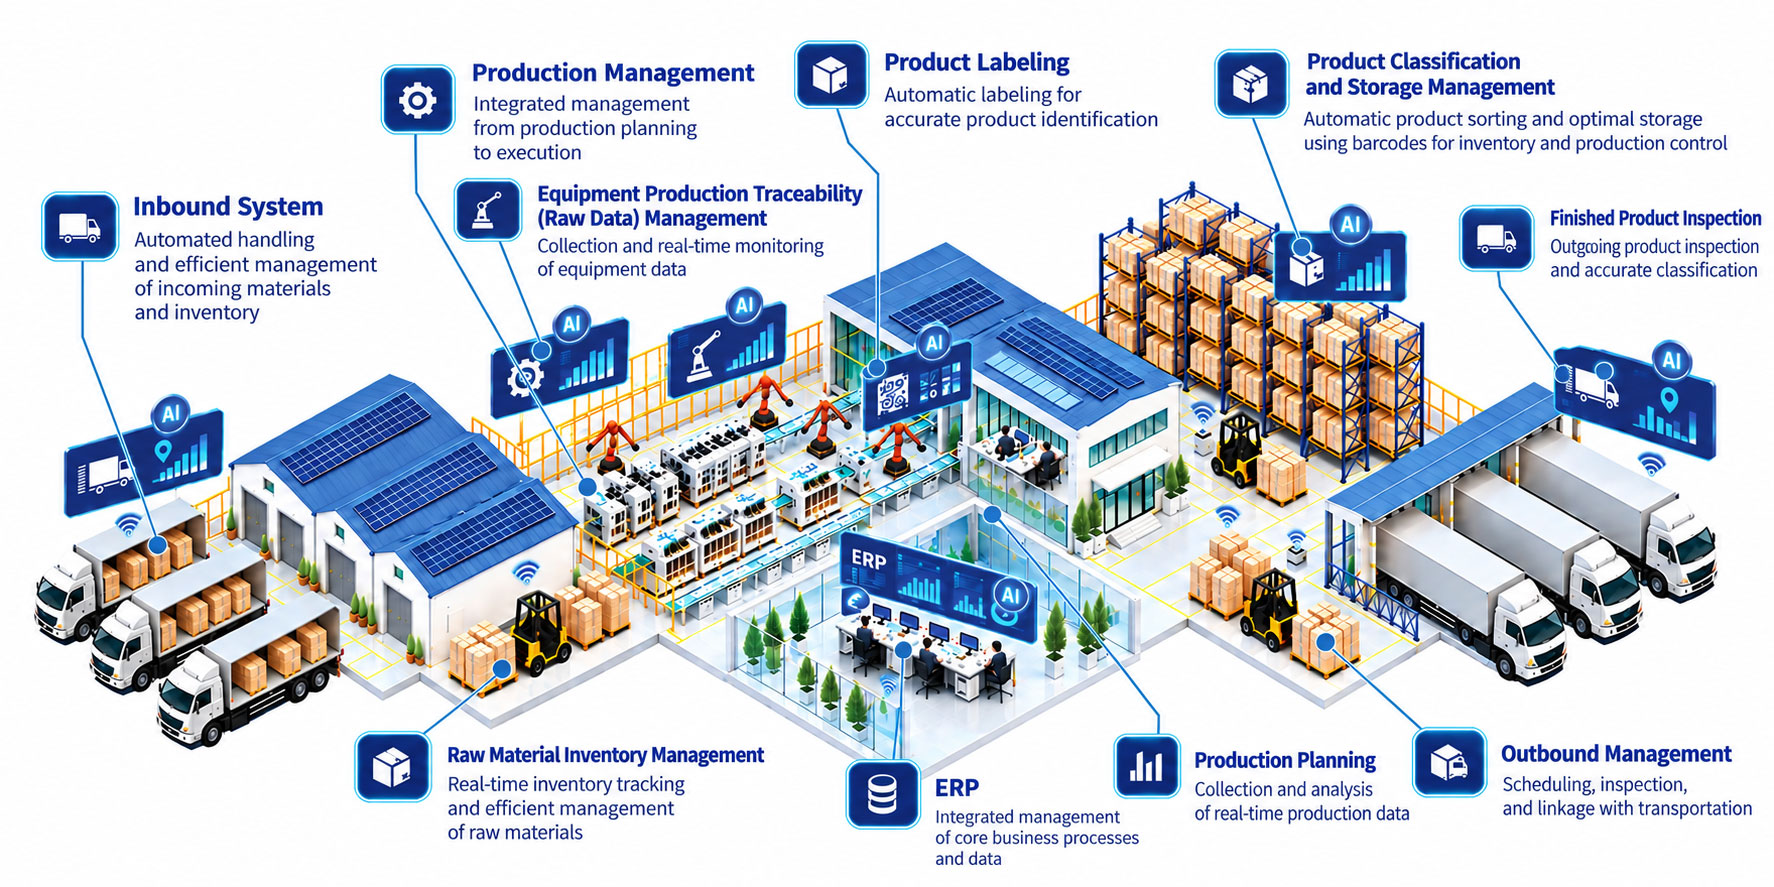
A smart factory uses sensors and integrated systems to collect and share data at every stage of the process, realizing automation and intelligence throughout manufacturing. This brings greater flexibility and efficiency than traditional manufacturing methods, along with benefits like lower production costs and faster responsiveness — and a smart factory encompasses a wide range of technologies to achieve it.
The global smart manufacturing technology market is projected to grow from $254.24 billion in 2022 to $787.54 billion by 2030. As a result, many manufacturers are moving away from traditional factory systems that haven't changed in decades and exploring new ways of operating — because doing so can strengthen the following business benefits even amid shifting customer expectations and economic uncertainty.
A smart factory is designed to reduce reactive, after-the-fact practices in favor of automated processes and intelligent systems that find and build the optimal workflow. Because production is optimized through real-time data even without human intervention, the savings in time and cost are substantial. It also helps produce more products efficiently through JIT (Just-In-Time) inventory management, accurate demand forecasting, and shorter production cycles. In fact, a 2019 Deloitte survey found that companies investing in smart factory initiatives saw performance improve by as much as 12% in areas such as manufacturing output, factory utilization, and labor productivity.
Smart factory technology monitors every manufacturing process and continuously improves product quality based on data. It minimizes redundant processes, reduces wasted time and materials, and minimizes downtime, enabling consistent production of high-quality products. A system that detects and resolves problems on its own — such as replenishing stock based on predicted conditions — also prevents product defects before they occur, minimizing the defect rate.
Less direct human involvement not only reduces labor costs, but minimizing redundant processes and downtime also boosts energy efficiency and cuts power consumption. It also shrinks the budget spent on product defects and wasted time and materials, and by predicting and preventing system faults, extends machine lifespan — lowering the overall cost of running the factory.
With a flexible manufacturing process, a smart factory can produce small batches of many product varieties tailored to individual customer needs, unlike the mass-production approach of a traditional factory. For the same reason, it responds quickly to shifting trends and supports customization, while system data analysis rapidly identifies weaknesses and drives improvement. This gives companies new business opportunities while playing a major role in securing a competitive edge in the market.
Another advantage of a smart factory is ensuring worker safety. Because a real-time monitoring system oversees the work environment, an alarm is sent immediately when a hazardous situation arises, or the problem is resolved automatically. According to a report from the International Society of Automation, robots and automated equipment can help eliminate 3 of the 5 leading causes of on-site injury. Building a safe work environment can help reduce the rate of industrial accidents.
A smart factory makes it far easier than before to establish eco-friendly manufacturing practices — using intelligent connectivity technology to reduce material waste and lowering carbon emissions by cutting defective products. Digital technologies such as blockchain and RFID (radio-frequency identification) can also trace the origin and transport of every material and supply, letting you manage product quality through ethical sourcing of materials.
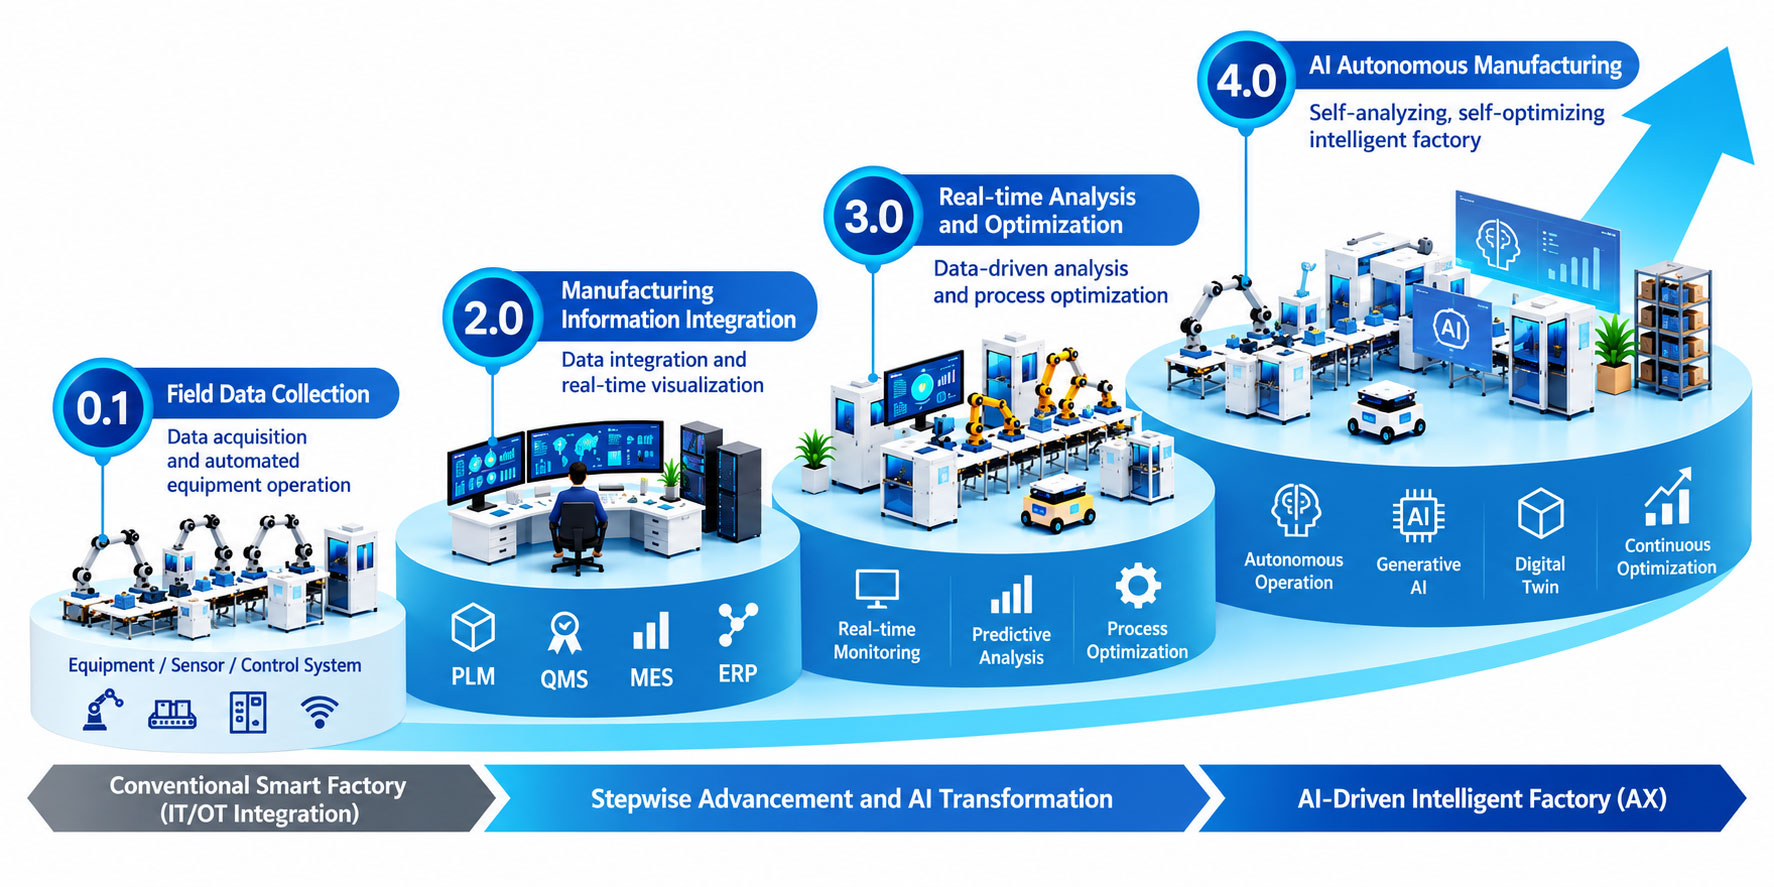
Depending on how extensively ICT is used and a company's capabilities, a smart factory's system smartification level is classified into five stages. A company can build up its smart factory in stages, according to its overall smart capability and operating capacity.
It's important to choose the level and features that fit a company's circumstances and focus there. In practice, many small and mid-sized enterprises build out the basic stage, since it's relatively affordable and easy to start with — and even at the basic stage, real-time aggregation and management of finished goods and material history management (lot tracking) are possible.
| Category | Field Automation | Factory Operations | Enterprise Resource Management | Product Development | Supply Chain Management |
|---|---|---|---|---|---|
| Advanced | IoT/IoS-Enabled | Cyberspace business (CPS) network collaboration |
|||
| IoT/IoS-enabled | IoT/IoS (modular) Big-data-based diagnostics and operation |
Big data/design·development, virtual simulation/3D printing |
|||
| Intermediate 2 | Automated equipment control | Automated equipment control | Real-time factory control | Simulation and end-to-end process automation |
Multi-product development collaboration |
| Intermediate 1 | Automatic equipment data aggregation | Automatic equipment data aggregation | Real-time decision-making | Automated technical-information generation and collaboration | Multi-product production collaboration |
| Basic | Automated performance aggregation | Automated performance aggregation | Process/logistics management (POP) | Server-based technical/delivery management | Reliant on a single parent company |
| No ICT Applied | Manual work | Manual work | Manual work | Manual work | Phone and email collaboration |
 Blog
 YouTube
 Naver TV
 Naver Clip